One retrofittable unit captures ash and SO₂ together — on a fraction of the water and footprint of a conventional scrubber — and turns the captured sulphur into ammonium-sulfate fertilizer you can sell.
Ash capture · certified in test, sustained in operation
Up to 95%
SO₂ removal — certified full-scale model testing
100,000+ h
Continuous field operation
0.25 L/m³
Closed-loop water use — a conventional wet scrubber uses 10–25 L/m³
Figures from certified full-scale testing and operator attestation in commercial operation.
The short version
Cleaner gas, lower cost — and a by-product that sells.
Lower capital cost
A fraction of a conventional scrubber island.5
Faster, cheaper install
Retrofits into existing housings — not a rebuild.
Lower running cost
Low energy and water; the by-product offsets cost.
Less water
Closed-loop — only 0.25 L/m³.1
Smaller footprint
Fits inside existing scrubber housings.
Sellable by-product
Sulphur leaves as fertilizer, not waste to dump.
The technology
One platform. Four pollutants. Three stages.
A modular wet scrubber that handles gas up to 180 °C with no pre-cooling, in a closed-loop, low-pressure-drop circuit.
Each stage is a modular cassette contour on the same platform — installed alone or in sequence, inside existing scrubber housings.
Proven in operation
Stage 1 · Ash
99.9% particulate capture, sustained over more than 100,000 hours on a commercial coal-fired boiler.
Proven in operation (SO₂)
Stage 2 · SO₂ + NOₓ
Up to 95% SO₂ removal in certified full-scale model testing. 86% sustained in commercial operation over 100,000+ hours in a retrofit constrained by the plant's existing housings and fans. Sulphur is recovered as certified ammonium-sulfate fertilizer rather than gypsum waste. The same contour has removed NOₓ at pilot scale. Pilot-tested
Pilot-tested
Stage 3 · CO₂
A CO₂-absorption contour built into the platform from the start and run at pilot scale, ready for the next development stage.
The complete platform
Proven over a decade of commercial operation — not a pilot.
NOₓ and CO₂ contours designed in and pilot-tested on the same architecture.
Complete engineering documentation, including a utility-commissioned 150 MW retrofit design.
Fig. 01 · Integration into an existing gas duct — inlet to stack
Performance path
From 86% to 97%+
The 86% retrofit figure is a site constraint, not a limit of the chemistry. The designers' roadmap:
86%
Single-stage retrofit
Proven in operation
Up to 95%
Full-scale model test
Certified model test
97–98.5%
Two-stage cascade
Calculated
Configuration ladder, not a timeline. Each figure is labelled by its evidence source.
Evidence
Measured, not asserted.
Headline figures backed by certified full-scale testing and operator attestation.
99.9%
Ash capture, certified in test and sustained in operation
Up to 95%
SO₂ removal — certified full-scale model testing
86% sustained in commercial operation over 100,000+ hours.
100,000+
hours
Continuous field operation
0.25
L/m³
Closed-loop water use — a conventional wet scrubber uses 10–25 L/m³
Certified full-scale test
State aerospace enterprise, 2011, signed acceptance act.
Complete seven-volume working project and cost estimate for a 150 MW retrofit (2014–2017).
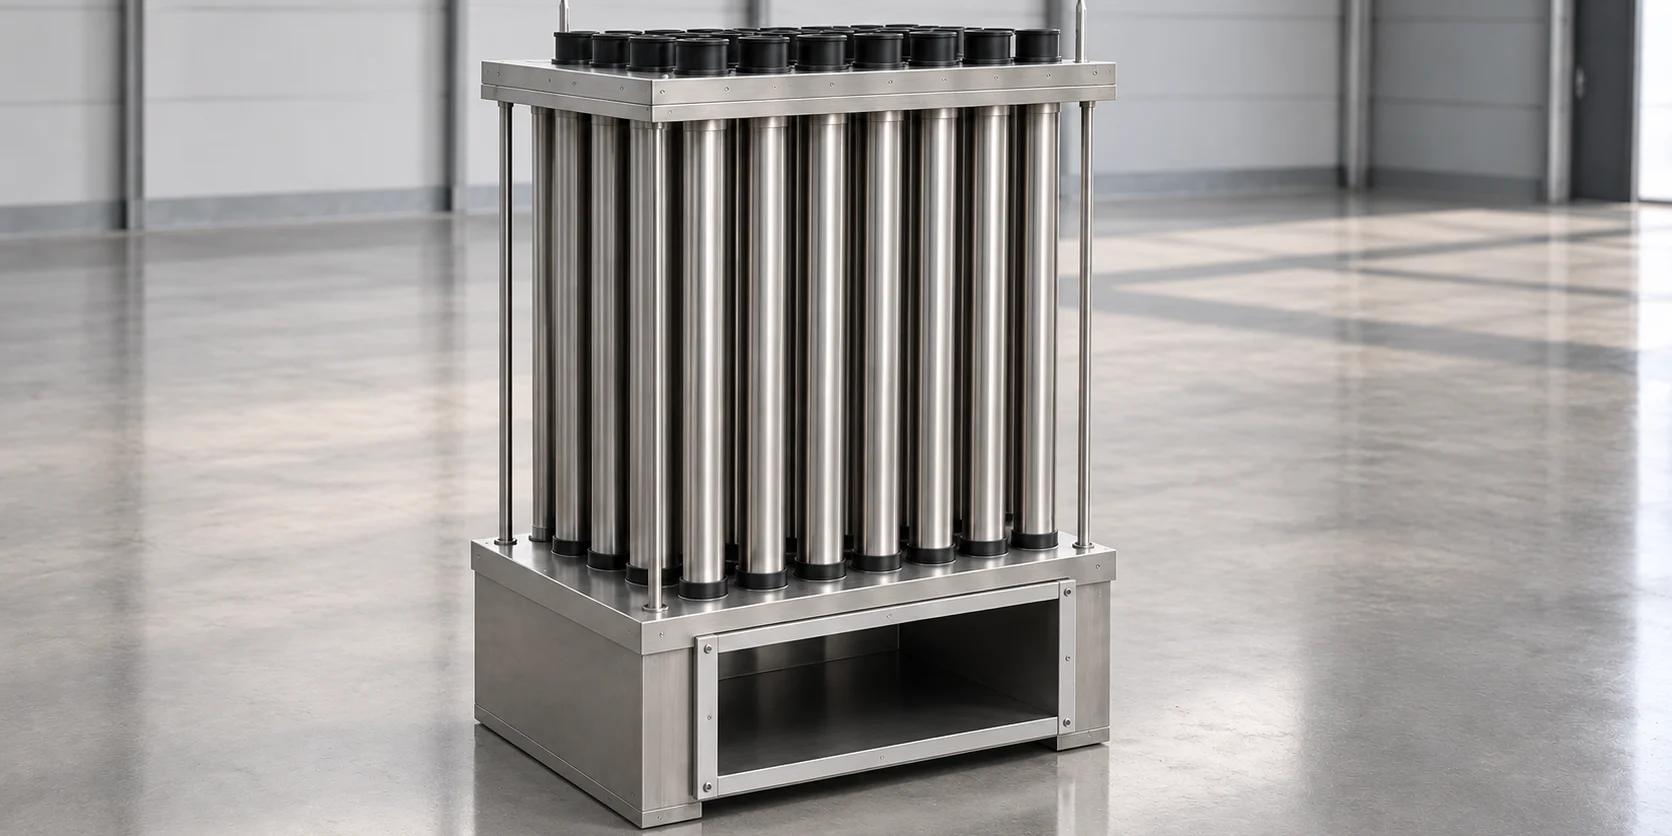
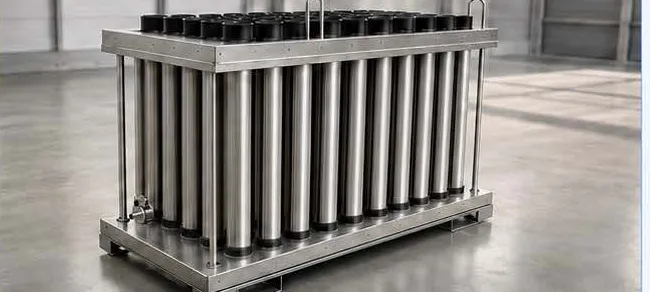
Fig. 02 · Assembled cassette module — tube bank mounted on its base housingFig. 03 · The tube elements — the vertical elements that make up each cassette
What is proven: 99.9% ash capture and up to 95% SO₂ removal in certified full-scale testing. In commercial operation, 86% SO₂ has been sustained across more than 100,000 hours. That 86% reflects a single-stage retrofit inside existing housings and fans — a configuration choice, not a limit of the chemistry. The designers' roadmap maps 90–93% with higher irrigation and pH control, and 97–98.5% in a two-stage cascade (both calculated). NOₓ and CO₂ are designed into the same platform and have run at pilot scale. Full test reports, design documentation and operating data are available under NDA.
How it compares
One unit doing the work of an ESP and a scrubber.
Conventional plants need three separate systems in series — a particulate device, an SO₂ scrubber, and an SCR reactor. Emulgator does ash and SO₂ in one retrofittable unit today, with NOₓ and CO₂ designed in and pilot-tested on the same platform.
Technology
Particulate (ash)
SO₂
NOₓ
CO₂
By-product
Water
Footprint
Emulgatorwet · proprietary reagent, no ammonia handling
99.9%1
86% retrofit (existing housings, existing fans) · up to 95% model test2
Designed in — same contour as SO₂ · pilot-tested3
Designed in — Stage 3 · pilot-tested3
Ammonium sulfate
Very low1
Compact / retrofit5
Wet FGD — limestonethe SO₂ incumbent
—
90–98%
—
—
Gypsum waste
High
Large
Wet FGD — ammoniaclosest chemistry analogue
—
>98%
—
—
Ammonium sulfate4
Low–moderate
Compact4
Dry / semi-dry FGDlime spray-dryer / CDS
—
80–95%
—
—
Dry waste
Low
Moderate
ESP / fabric filterparticulate only
>99%
—
—
—
Ash
None (dry)
Large
SCR / SNCRNOₓ only
—
—
—
—
None
Reactor + catalyst
1 Ash capture and water use are independently tested and measured in field operation.2 The 86% figure reflects a single-stage retrofit installed inside the plant's existing housings and fans — a site constraint, not a limit of the technology. SO₂ removal is operator-attested at 86% in single-stage retrofit operation and certified at up to 95% in full-scale model testing; a two-stage cascade is calculated at 97–98.5%. Emulgator's advantage is integration, footprint, water, the sellable by-product and capital cost in one retrofittable unit.3 NOₓ and CO₂ contours were built and run at pilot scale in a three-stage test programme alongside the ash and SO₂ stages; results are available under NDA.4 Ammonia FGD also yields ammonium sulfate and can be compact; the Emulgator reagent requires no ammonia storage or handling.5 Capital cost is documented in a utility-commissioned 2016 retrofit estimate for a 150 MW unit; footprint figures are owner-stated. Removal efficiencies are typical ranges and vary by site, fuel and configuration.
Where it fits
Built for heavy industry.
Wherever high-sulphur fuel or dust-laden off-gas meets tightening limits and a need to retrofit.
Power & heat
Coal- and lignite-fired boilers facing SO₂ and particulate limits.
Steel & cement
Sinter plants, coke ovens and kilns with high-SO₂ off-gas.
Refining & process
Process furnaces and industrial off-gas where space and water are tight.
Fig. 04 · Industrial gas-cleaning installation
About
Engineered in-house, proven in the field.
Emulgator is the work of two Ukrainian engineers whose careers began in the aerospace industry. The engineer who designed it brought that discipline to flue-gas cleaning: the system he designed has run for more than 100,000 hours on a commercial coal-fired boiler, and he led the detailed engineering of a utility-commissioned 150 MW retrofit. His commercial partner has directed the technology's development and its route to market. The cassettes were manufactured at an aerospace-grade state enterprise.
Since 2011
R&D and field testing
100,000+ h
In real operation
150 MW
Utility-commissioned retrofit design
Contact
Let's talk.
We work with power producers, industrial operators and technology partners on retrofits, pilots and licensing.